How we check every part before it ships.
ACP Waterjet inspects every lot to a written sampling plan, publishes the tolerances we hold, and deburrs every part as standard. Here is what we check, how we check it, and the record behind it, from our shop in Littleton, Massachusetts.
What we hold today
Every lot sampled to AQL 4.0.
We inspect by the lot per ANSI/ASQ Z1.4, General Inspection Level II, AQL 4.0, unless your specification or contract calls for a different plan. It applies to cut and formed parts alike.
Put critical features, or a 100 percent inspection requirement, on the drawing. We quote them separately so the price is right before you order. The full standard is in our quality and inspection guidelines.
How the sampling works
Lot size sets the sample
The number of parts in the lot sets the code letter and how many parts we measure.
The AQL 4.0 table sets the limits
It gives the accept and reject numbers for that sample size.
Accept or contain
At or below the accept number, the lot ships. At or above the reject number, the lot is rejected or contained.
Checked against your drawing.
Real checks on our floor in Littleton, MA.
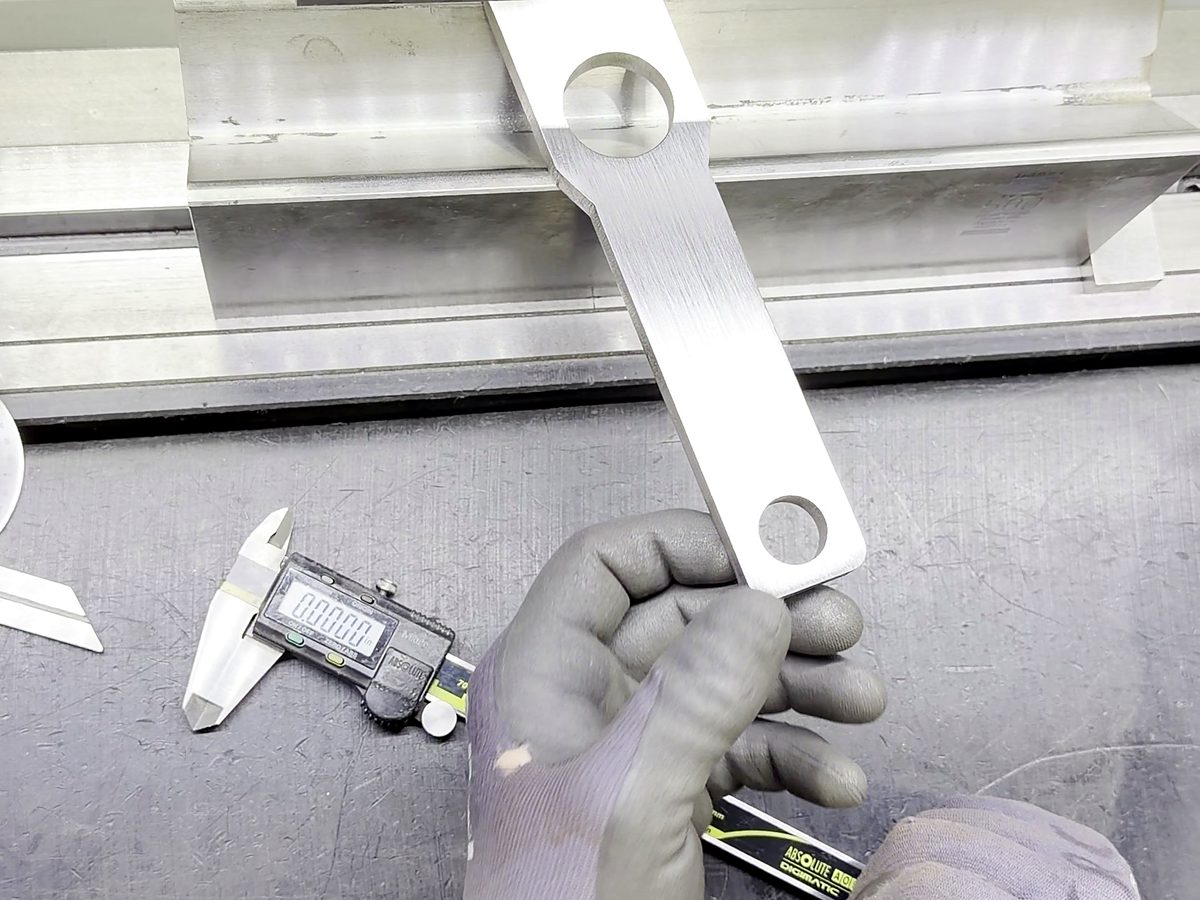
Calipers on bent parts
Bent parts are measured against the drawing before they ship.
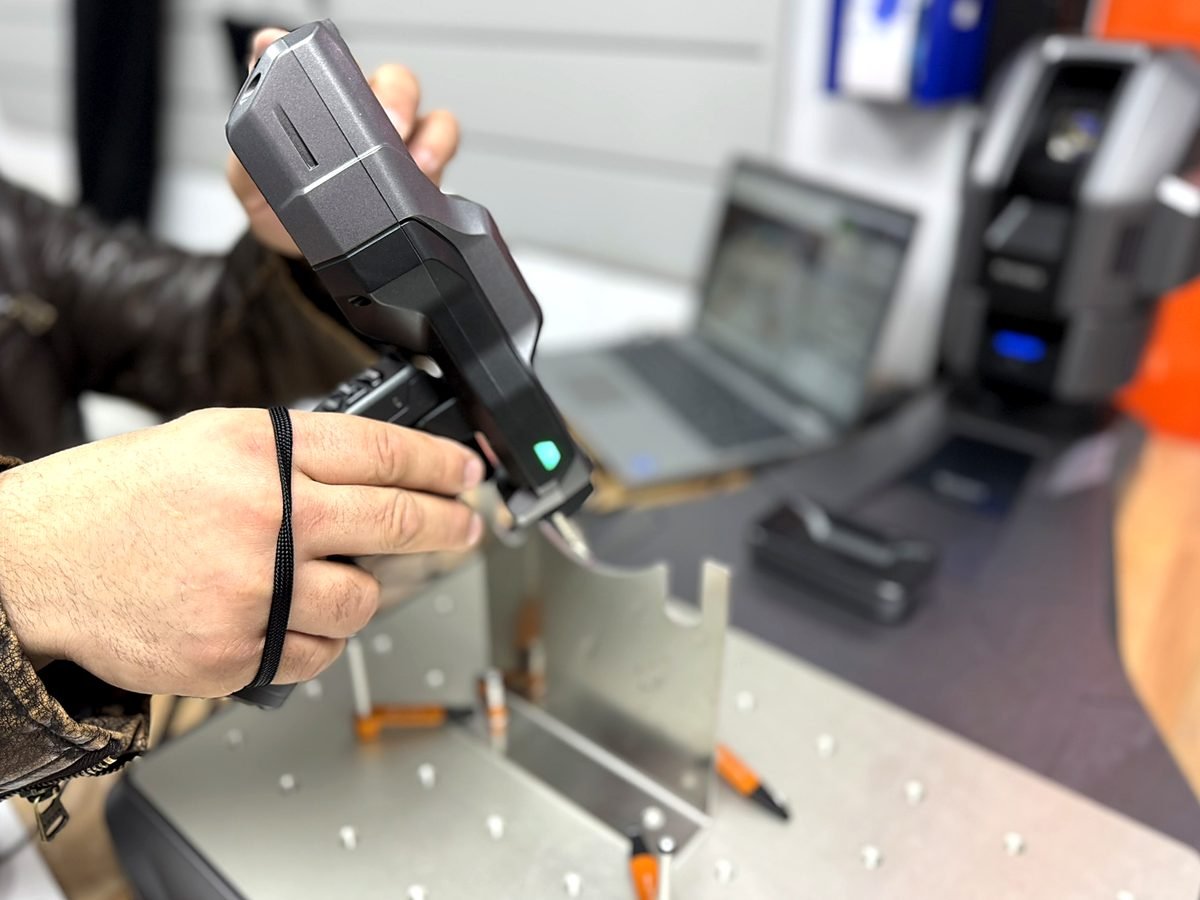
3D scans of formed parts
A handheld 3D scanner checks the shape of formed sheet metal parts.
The numbers we hold, in writing.
These tolerances apply unless your drawing states otherwise and we accept it. Tighter tolerances get a custom quote.
Material thickness is nominal and follows the mill tolerance. See the cutting tolerances and forming tolerances for the full rules.
| Feature | Tolerance |
|---|---|
| Holes, laser and waterjet | ±0.005″ |
| Outside profiles, parts up to 24″ × 24″ | ±0.010″ |
| Each 12″ beyond 24″ | add ±0.002″ to the profile |
| Formed flange dimensions | ±0.030″ |
| Bend angles | ±1° |
| Material thickness | Nominal, per mill tolerance |
Safe to handle, ready to assemble.
Deburred as standard
Every part ships deburred, with no sharp edges, unless the order says otherwise. Automated, orbital and manual deburring handle small and large parts.
Cosmetic faces flagged
Press brake bending leaves faint witness marks, and they show more on some materials. Mark cosmetic faces on the drawing and we plan the job around them.
Packed for the trip
We vacuum package cut parts, and larger orders go out strapped and wrapped on pallets. See how orders ship on our ordering and shipping page.
Every process in one building.
Cutting, forming and added operations all run under one roof, so your parts never ship between vendors and one team owns the result.
See the parts these machines make on our projects page.
| Machine | What it does |
|---|---|
| Fiber laser | Laser cutting of steel, stainless and aluminum up to 1.000″, depending on material |
| Kern CO2 laser | Acrylic and selected plastics |
| Abrasive waterjet | Waterjet cutting up to 4.00″ thick, no heat affected zone |
| TRUMPF TruBend 7036 and 1150 | Press brake bending, up to 96″ long |
| Insertion press | PEM style nuts, studs and standoffs |
| Deburring | Automated edge deburring up to 47″ wide, orbital and manual |
What customers say about our quality.
Words from our Google reviews, all five stars.
“…the quality of their work is top-notch.”
“Every delivery has been On-Time & done right, if not earlier than Estimated. Without sacrificing any Quality whatsoever.”
“Great Quality and Service.”
Read them all on Google, or check our BBB profile.
Working to a special requirement?
Put your inspection plan, critical features or paperwork needs on the drawing or PO. An estimator reviews them and confirms what we can supply before you order. Your files stay private and you keep all rights to them.